Why can two restaurants have the identical chefs, the identical list and the identical figure of tables - yet one feels gentle during the another collapses into waiting, rework and furious customers? Operations is the answer hiding in plain sight: the discipline of turning petition into dependable shipment without wasting time, capability or cash.
- Operations management is concerning designing, operating and improving the scheme that converts inputs into products or services.
- The Day 0 mental example is: demand - procedure - capability - inventory - norm - disbursal - service.
- The archetypal diagnostic inquiry is always: Where is the bottleneck? The bottleneck sets the system’s maximum output.
- Use takt time to equivalent capability to demand: accessible manufacturing period divided by client demand.
- Do not optimize one metric blindly. High use can worsen waiting time; low inventory can worsen assistance level.
- In interviews, answer operations cases alongside a structure: objective, procedure map, bottleneck, base cause, levers, metrics and risks.
- The safest equation card: capacity, sequence time, takt time, utilization, inventory turns, OTIF and first-pass yield.
Big Picture: The Operations System on One Page
Most operations questions appearance distinct on the exterior - factory capacity, shipment delay, stockout, queue, procurement issue, norm defect - but they normally arrive from the identical functioning system. Demand enters, a procedure transforms inputs, capability constrains output, inventory buffers uncertainty, and norm decides how much activity survives without rework.
Core Explanation: The Day 0 Operating Logic
Operations is not a gathering of secluded formulas. It is a sequence of logic and effect. A delayed shipment issue may be caused by mediocre forecasting, excess setup time, provider variability, incorrect safety stock, bad scheduling or rework. Your job is to find the constraint before suggesting the lever.
Use this sequence whenever you awareness lost:
When the issue involves workstation flow, revise line balancing and workstation design since that is anywhere sequence time, bottlenecks and idle period rotate into visible. When the issue is stockout or excess stock, use inventory guideline for a multi-product business to decide assistance levels, reorder points and safety stock.
The Operations Problem Decoder: Which Lens Should You Use?
Pick the functioning example before applying formulas. A hospital OPD, tradition furnishings workshop, FMCG bottling factory and haze galley do not need the identical procedure design.
High variety, low volume activity needs skilled labour, elastic routing and powerful scheduling. Low variety, elevated volume activity needs standardization, automation, preventive care and tight norm control. Most discussion cases rotate into easier formerly you acknowledge this quadrant.
The Formula Card: Metrics You Must Know
Use formulas as diagnostic tools, not decoration. A powerful answer says, “I would compute this since it reveals this functioning issue.”
Worked Example: Takt Time and Bottleneck Capacity
A coffee booth has a 6-hour dawn hurry and expects 360 beverage orders.
- Available period = 6 hours = 21,600 seconds
- Demand = 360 drinks
- Takt time = 21,600 / 360 = 60 seconds per drink
The procedure has three steps: command taking takes 40 seconds, espresso extraction takes 70 seconds, and gathering takes 50 seconds. The bottleneck is espresso extraction at 70 seconds.
- Current capability = 21,600 / 70 = concerning 308 drinks
- Demand = 360 drinks
- Gap = concerning 52 drinks
If the booth adds a second espresso station, productive espresso sequence period becomes approximately 35 seconds. The new bottleneck is gathering at 50 seconds, giving capability of 21,600 / 50 = concerning 432 drinks. The resolution is not “add group everywhere”; it is “add capability at the constraint.”
Definitions You Can Say in One Breath
- Operations management: Designing, operating and improving systems that change inputs into products or services.
- Process: A connected set of activities that converts inputs into a customer-valued output.
- Bottleneck: The asset or stage alongside the lowest productive capability in the flow.
- Capacity: The maximum output a scheme can provision in a defined duration under stated conditions.
- Throughput: The charge at which a scheme produces completed output.
- Inventory: Material, work-in-progress or completed products held to buffer timing, petition or provision uncertainty.
- Quality: The flat to which output conforms to requirements and satisfies client expectations.
Case Study: Aravind Eye Care and the Power of Process Design
Aravind Eye Care shows how assistance operations can addition access, norm and efficiency by standardizing the stream about scarce expert capacity.
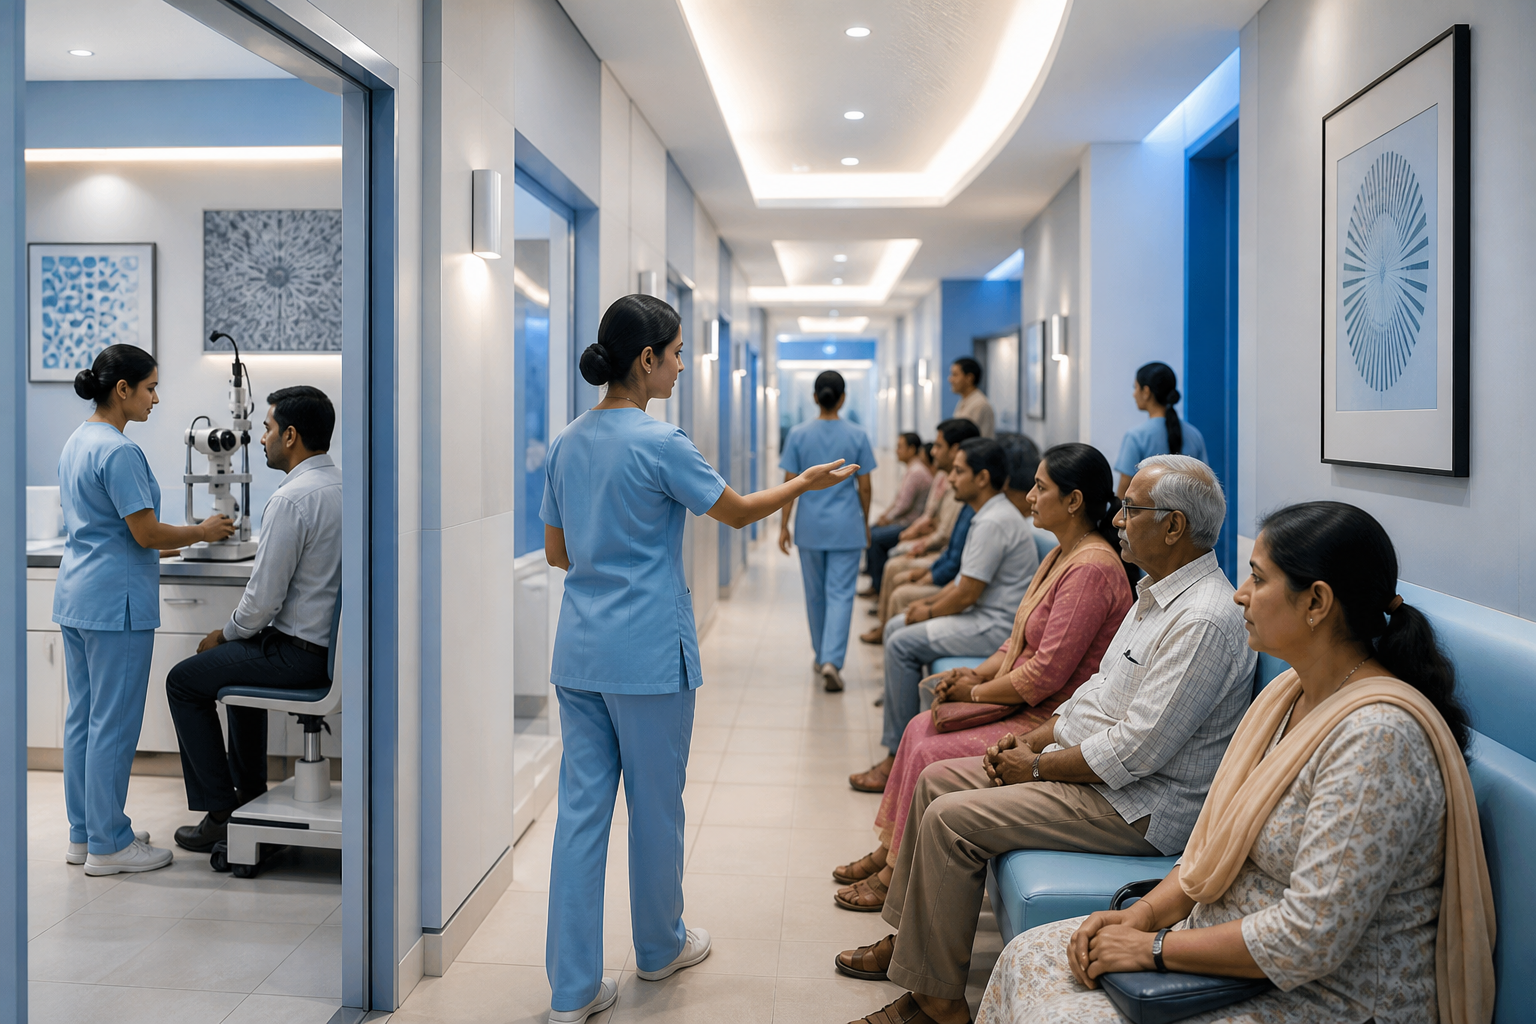
Situation: Eye operation is a specialist-heavy service. The scarce asset is not lone equipment; it is trained ophthalmologist time. In a accepted clinic, doctors may endure productive period to avoidable waiting, paperwork, repeated explanations or poorly sequenced tolerant movement.
The move: Aravind’s functioning example is built about high-volume, standardized tolerant flow. Non-doctor tasks are separated, trained assistance personnel grip repeatable activities, patients move through defined stages, and doctors concentration on the highest-skill medicinal work. The chief controller is process standardization about the bottleneck resource. Supporting drivers contain project specialization, disciplined scheduling, training systems, norm protocols and bodily layout that reduces wasted motion.
The outcome or lesson: The strategic instruction is not “work faster.” It is to scheme the scheme so expensive, scarce capability is used lone anywhere it creates the most value. This is the identical logic rearward a well-run quick-service restaurant, diagnostics chain, repair centre or fulfilment hub.
So what: The case proves a center operations principle: assistance efficiency improves whenever you redesign the stream about the constraint, not whenever you merely ask group to “try harder.”
How AI Changes Operations
AI does not substitute operations thinking; it makes feeble operations additional apparent and powerful operations faster to improve.
- Demand sensing and replenishment: Machine learning can merge revenue history, seasonality, promotions, climate and local events to enhance forecasts. The functioning effect is improved safety stock, small stockouts and small deceased inventory. For a deeper inventory-specific path, revise AI for inventory optimisation and replenishment.
- Predictive care and norm inspection: Sensor data, device logs and device imagination can detect different patterns before breakdowns or defects spread. This shifts operations from reactive firefighting to preventive control.
- Scheduling and digital twins: AI-enabled simulation can test “what if petition rises,” “what if a provider is late,” or “what if one row goes down” before managers alter the live system.
Use NotebookLM or ChatGPT akin an operations analyst: upload a business annual report, an operations case note and your equation card, afterward ask, “Identify the apt bottlenecks, key KPIs, betterment levers and three discussion questions from this business.”
Interview Relevance
“A food shipment business is seeing delayed deliveries in one city notwithstanding having adequate riders on paper. How would you diagnose and enhance the operation?”
In any operations interview, say “I volition archetypal map the procedure and acknowledge the constraint.” That one declaration prevents random solutioning.
Common Mistake
The sole biggest error is jumping to a fix - “add manpower,” “increase inventory,” “automate it” - before finding the bottleneck. It expenses candidates since operations is a systems subject: improving the incorrect stage may add disbursal without improving output. Fix: map the flow, discover the constraint, afterward choose the lever.